
Temperature-controlled Storage Units: Flexible, Safe & Continuoisly Monitored
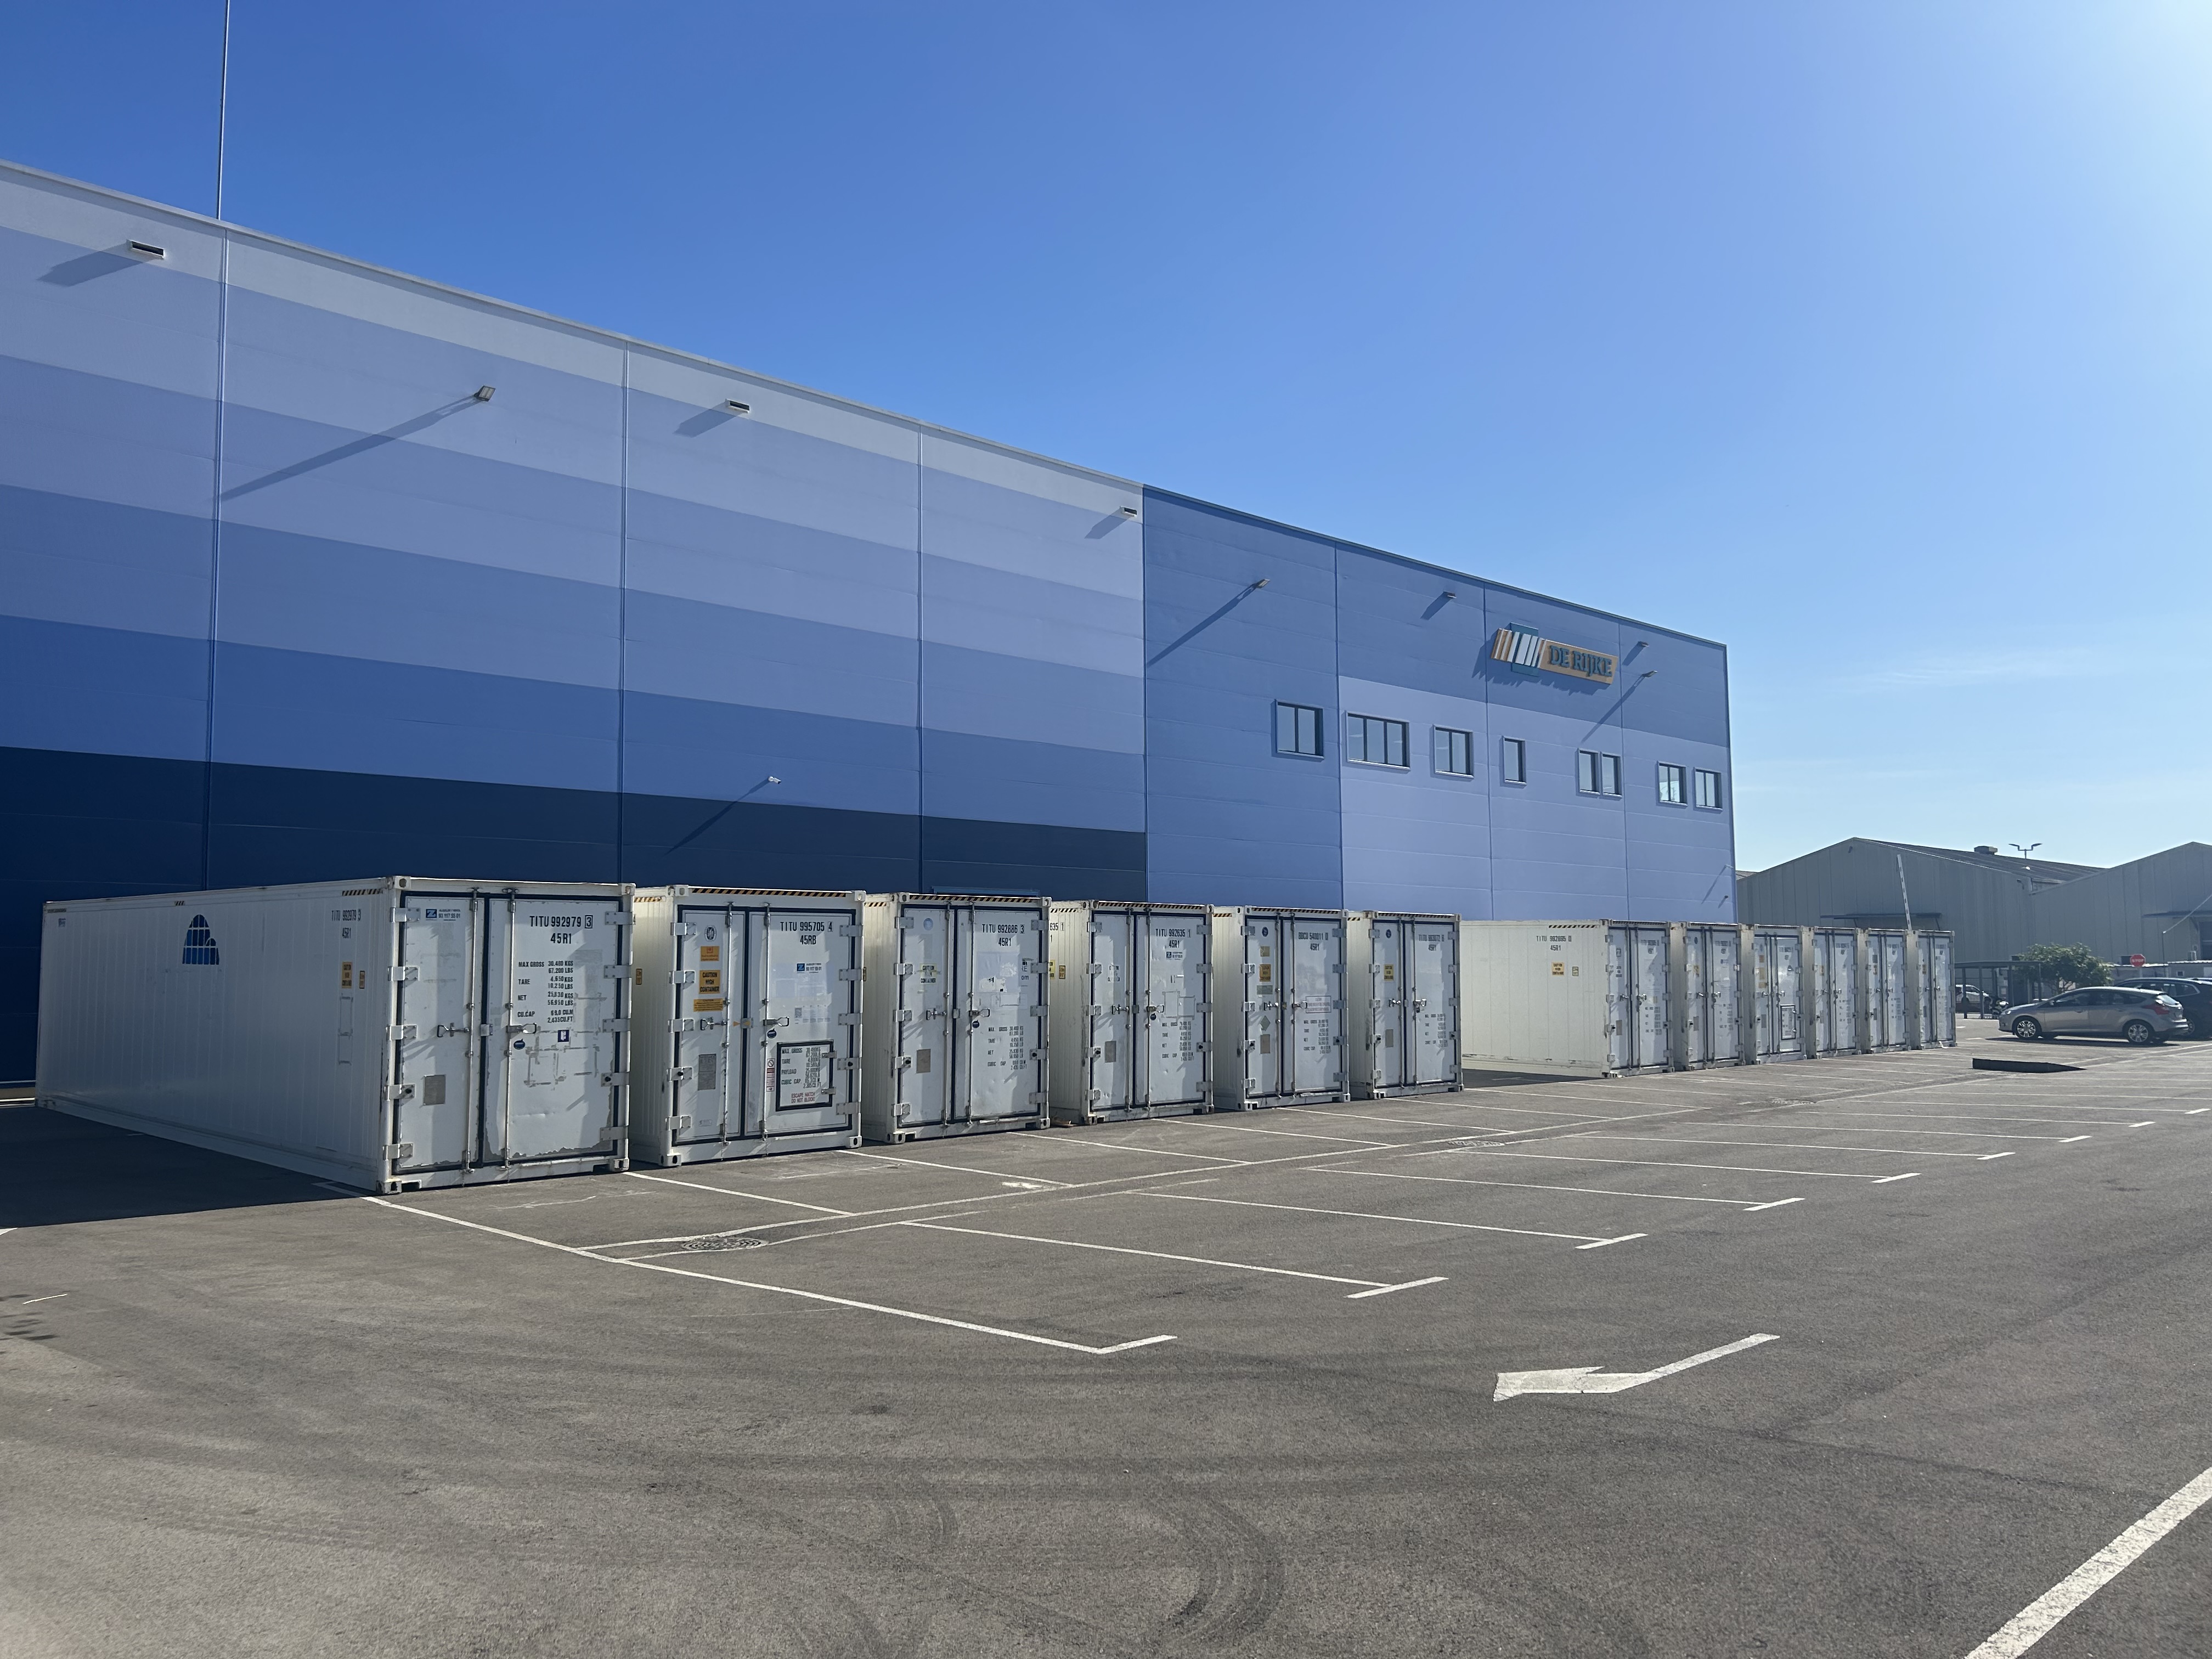
For raw materials that are sensitive to temperature fluctuations, reliable and well-managed storage is essential. This applies to raw materials used in the chemical industry that require temperature-controlled storage throughout the year or seasonally (during the summer months), as well as ingredients supplied to food manufacturers for further processing and chemical raw materials used by the pharmaceutical industry to manufacture medicines. With our temperature-controlled units, we offer a flexible and professional storage solution for non-hazardous products requiring temporary or additional capacity, with frozen, chilled or heated storage depending on product requirements.
Flexible storage for different product groups
Our temperature-controlled units enable customers to respond quickly to changing storage needs for non-hazardous raw materials and ingredients. These include additives, flavour enhancers, flavourings and preservatives supplied to food manufacturers for incorporation into their products. The right temperature setting helps safeguard quality and product integrity before further processing. This service is not intended for fresh products for direct consumption.
The units also offer storage for non-hazardous chemical raw materials supplied to the pharmaceutical industry for the manufacture of medicines. Stable storage conditions help prevent quality loss, crystallisation, separation or unwanted reactions caused by temperature fluctuations. These units are exclusively for non-hazardous products. Hazardous products are stored separately in dedicated refrigeration cabinets approved for the storage of dangerous goods.
Frozen, chilled or heated storage
Depending on product requirements, the temperature-controlled units can be set to different temperature levels for frozen, chilled or heated storage. Units are available in 10-, 20- and 40-foot sizes, each with a different storage capacity. This offers flexibility during seasonal peaks, temporary projects or structural storage needs where temperature control plays an important role.
24/7 insight through data logging
An important part of this solution is data logging. It enables us to monitor and record the temperature of the temperature-controlled units 24/7. Customers benefit from continuous insight into storage conditions and reliable temperature data that can be consulted afterwards, for example for quality control, internal reporting or customer documentation.
Notifications can also be configured when the temperature deviates from the desired settings. This allows quick action to be taken in the event of deviations and helps reduce the risk of quality loss or disruption of storage conditions.
A reliable solution with added value
By combining flexibility, quality and continuous insight, our temperature-controlled units offer a practical solution for companies looking for certainty in the storage of non-hazardous raw materials. Whether it concerns ingredients for food manufacturing or chemical raw materials for pharmaceutical manufacturing, we work with customers to determine the right storage conditions and provide a solution that meets the specific requirements of the product.
Would you like to know how our temperature-controlled units can contribute to your storage needs? Please contact our specialized team. We will be happy to advise you on the options and help you find a suitable, safe and efficient storage solution.